The thickness figure gets specified to two decimal places; weight at 180-420 gsm is the one that decides whether the lot is usable.
3D mesh: why the headline number is the least useful one
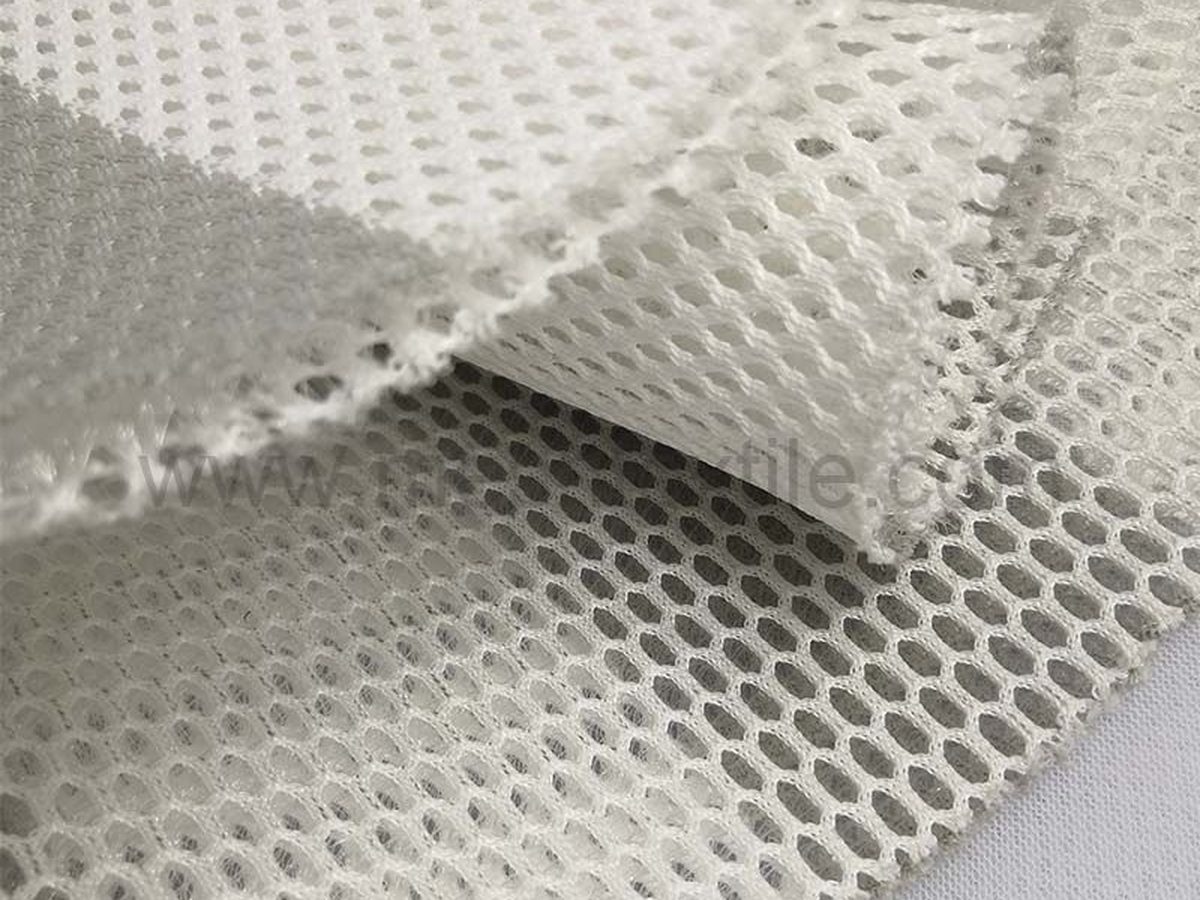
Every quotation leads with thickness. It is easy to compare and it is the number the factory can hit most cheaply. But it tells you almost nothing on its own: thickness sets the frame, and the parameters below set whether the product survives its first year in service. A buyer who compares only the headline figure is buying a sample, not a supply agreement.
For 3D mesh, the practical rule is to fix the headline figure at the level your product needs and then spend your negotiating attention on compression recovery and air permeability. Those two are where cheap goods differ from adequate goods, and they are usually absent from the quotation sheet.

The 3D mesh numbers that decide performance
| Parameter | Typical range | What it changes | Thickness | 3-15 mm | Cushioning and airflow. Above 8 mm cutting, edge binding and sewing all get harder and reject rates rise. | Weight | 180-420 gsm | Durability and cost. Under 220 gsm in seating, expect compression set within a season. | Compression recovery | >= 90 % | The single best predictor of whether a seat still looks new after a year of use. | Air permeability | 300-1200 L/m2/s | Breathability claim. A dense surface layer can halve this without changing thickness. | Monofilament diameter | 0.08-0.20 mm | Sets the resilience of the gap. Thin monofilament feels soft and collapses early. | Usable width | 150-160 cm | Affects cutting yield on bag panels and chair covers more than price per metre does. | Surface construction | tricot / plain / mesh | Tricot resists snagging; open mesh looks technical but catches on Velcro and zips. | Colour fastness to rubbing; measured on thickness, 3-15 mm | >= grade 4 | Dark shades on light foam show crocking at fold lines after packing. |
|---|
Read the table as a set of trade-offs rather than a checklist. Moving any single line usually costs money somewhere else, and the cheapest way to hit one figure is often to let another slip.
Thickness
Typical range: 3-15 mm. Cushioning and airflow. Above 8 mm cutting, edge binding and sewing all get harder and reject rates rise.
Weight
Typical range: 180-420 gsm. Durability and cost. Under 220 gsm in seating, expect compression set within a season.
Compression recovery
Typical range: >= 90 %. The single best predictor of whether a seat still looks new after a year of use.
Air permeability
Typical range: 300-1200 L/m2/s. Breathability claim. A dense surface layer can halve this without changing thickness.
Monofilament diameter
Typical range: 0.08-0.20 mm. Sets the resilience of the gap. Thin monofilament feels soft and collapses early.
Compression recovery: range, tolerance and the clause
It also explains why compression recovery is the first line a buyer loosens and the last line a claim refers to.

What >= 90 % does not tell you
| Position | Value | Effect on 3D mesh | Where it shows up | Floor | >= 90 % | Lowest cost, least margin for process variation; held at thickness, 3-15 mm | Snagging and pilling within a season | Working middle | >= 90 % | Predictable performance at a normal price; read against thickness, 3-15 mm | Nothing to negotiate, nothing to explain; written as thickness 3-15 mm | Ceiling | >= 90 % | Best performance, highest cost; measured on thickness, 3-15 mm | Cost the end product may not recover; held at thickness, 3-15 mm |
|---|
The figure that decides the outcome is not compression recovery itself but the tolerance around it. A supplier who quotes >= 90 % without a tolerance has not quoted a specification, and the first lot will define the tolerance for you.
How to measure compression recovery
The reference method here is Pilling, run to ISO 12945-2, with an acceptance of >= grade 3-4.
Condition the sample before measuring. Results in this family move by 10-20 % between a dry laboratory and a humid one, and two labs can disagree on the same material without either being wrong.
A marginal pass on compression recovery tells you the process is running at the edge, which is the information you need before the next lot rather than after it.
The clause to write for compression recovery
Compression recovery appears with a tolerance and a test, not as a standalone number.
The clause that protects you is not the value, it is the sentence that says what happens when the value is missed. Put it in the purchase order, not only in the enquiry.
Air permeability: range, tolerance and the clause
It also explains why air permeability is the first line a buyer loosens and the last line a claim refers to.
What 300-1200 L/m2/s does not tell you
| Position | Value | Effect on 3D mesh | Where it shows up | Floor | 300 | Lowest cost, least margin for process variation; read against thickness, 3-15 mm | Odour after washing within a season | Working middle | 300-1200 L/m2/s | Predictable performance at a normal price; written as thickness 3-15 mm | Nothing to negotiate, nothing to explain; measured on thickness, 3-15 mm | Ceiling | 1200 L/m2/s | Best performance, highest cost; held at thickness, 3-15 mm | Cost the end product may not recover; read against thickness, 3-15 mm |
|---|
The figure that decides the outcome is not air permeability itself but the tolerance around it. A supplier who quotes 300-1200 L/m2/s without a tolerance has not quoted a specification, and the first lot will define the tolerance for you.
How to measure air permeability
The reference method here is Colour fastness to rubbing, run to ISO 105-X12, with an acceptance of >= grade 4 dry, >= 3-4 wet.
Take samples from the beginning, middle and end of the run. A single sample from the top of a roll tells you about the top of that roll, and air permeability varies more across a run than most buyers expect.
A marginal pass on air permeability tells you the process is running at the edge, which is the information you need before the next lot rather than after it.
The clause to write for air permeability
Air permeability appears with a tolerance and a test, not as a standalone number.
Monofilament diameter: range, tolerance and the clause
Sets the resilience of the gap. Thin monofilament feels soft and collapses early.
That makes it a design decision rather than a purchasing one, which is why changing it after the product is fixed costs more than changing the material.
What 0.08-0.20 mm does not tell you
| Position | Value | Effect on 3D mesh | Where it shows up | Floor | 0.08 | Lowest cost, least margin for process variation; written as thickness 3-15 mm | Compression set within a season | Working middle | 0.08-0.20 mm | Predictable performance at a normal price; measured on thickness, 3-15 mm | Nothing to negotiate, nothing to explain; held at thickness, 3-15 mm | Ceiling | 0.20 mm | Best performance, highest cost; read against thickness, 3-15 mm | Cost the end product may not recover; written as thickness 3-15 mm |
|---|
Specifying the ceiling is only justified when the end product carries a warranty that would be expensive to honour. Otherwise it is cost without a customer-visible benefit.
The figure that decides the outcome is not monofilament diameter itself but the tolerance around it. A supplier who quotes 0.08-0.20 mm without a tolerance has not quoted a specification, and the first lot will define the tolerance for you.
How to measure monofilament diameter
The reference method here is Dimensional change, run to ISO 6330 / ISO 5077, with an acceptance of <= 3 %.
Measure on the goods as delivered, not on the greige or the pre-finished material. The figure that matters is the one in the product your customer receives.
A marginal pass on monofilament diameter tells you the process is running at the edge, which is the information you need before the next lot rather than after it.
The clause to write for monofilament diameter
Monofilament diameter appears with a tolerance and a test, not as a standalone number.
The clause that protects you is not the value, it is the sentence that says what happens when the value is missed. Put it in the purchase order, not only in the enquiry.
Thickness on 3D mesh: range, tolerance and the clause
It also explains why thickness is the first line a buyer loosens and the last line a claim refers to.
For 3D mesh fabric, the working range is 3-15 mm. Inside that band the choice is commercial; outside it, the product changes category and so does the price.
What 3-15 mm does not tell you
| Position | Value | Effect on 3D mesh | Where it shows up | Floor | 3 | Lowest cost, least margin for process variation; measured on thickness, 3-15 mm | Compression set within a season | Working middle | 3-15 mm | Predictable performance at a normal price; held at thickness, 3-15 mm | Nothing to negotiate, nothing to explain; read against thickness, 3-15 mm | Ceiling | 15 mm | Best performance, highest cost; written as thickness 3-15 mm | Cost the end product may not recover; measured on thickness, 3-15 mm |
|---|
Buyers default to the floor because it is the cheapest compliant answer. That is rational until the first claim, and then the saving is measured against a replacement shipment.
The figure that decides the outcome is not thickness itself but the tolerance around it. A supplier who quotes 3-15 mm without a tolerance has not quoted a specification, and the first lot will define the tolerance for you.
How to measure thickness on 3D mesh
The reference method here is Compression recovery, run to internal 5 kg / 24 h / 40 C, with an acceptance of >= 90 %. The method is the easy part; sampling and conditioning are where reports diverge.
Take samples from the beginning, middle and end of the run. A single sample from the top of a roll tells you about the top of that roll, and thickness varies more across a run than most buyers expect.
Record the measured value rather than pass or fail. A marginal pass on thickness tells you the process is running at the edge, which is the information you need before the next lot rather than after it.
The clause to write for thickness on 3D mesh
The line below is the version we can quote against without inventing anything. Thickness appears with a tolerance and a test, not as a standalone number.
3D spacer mesh, 100 % polyester, 6 mm, 320 gsm, 155 cm usable, compression recovery >= 90 %, laminated to 2 mm PU foam with hot-melt adhesive, Pantone 19-4013 TCX
Write it once and reuse it. The buyers who avoid claims are not stricter than everyone else; they send the same well-written clause every time.
Weight on 3D mesh: range, tolerance and the clause
The consequence is that this figure sets the floor for everything downstream: the process, the price and the failure mode all follow from it.
For 3D mesh fabric, the working range is 180-420 gsm. Inside that band the choice is commercial; outside it, the product changes category and so does the price.
What 180-420 gsm does not tell you
| Position | Value | Effect on 3D mesh | Where it shows up | Floor | 180 | Lowest cost, least margin for process variation; held at thickness, 3-15 mm | Delamination within a season | Working middle | 180-420 gsm | Predictable performance at a normal price; read against thickness, 3-15 mm | Nothing to negotiate, nothing to explain; written as thickness 3-15 mm | Ceiling | 420 gsm | Best performance, highest cost; measured on thickness, 3-15 mm | Cost the end product may not recover; held at thickness, 3-15 mm |
|---|
Buyers default to the floor because it is the cheapest compliant answer. That is rational until the first claim, and then the saving is measured against a replacement shipment.
The figure that decides the outcome is not weight itself but the tolerance around it. A supplier who quotes 180-420 gsm without a tolerance has not quoted a specification, and the first lot will define the tolerance for you.
How to measure weight on 3D mesh
The reference method here is Peel strength (laminated), run to ISO 2411, with an acceptance of >= 6 N/50 mm. The method is the easy part; sampling and conditioning are where reports diverge.
Measure on the goods as delivered, not on the greige or the pre-finished material. The figure that matters is the one in the product your customer receives.
Record the measured value rather than pass or fail. A marginal pass on weight tells you the process is running at the edge, which is the information you need before the next lot rather than after it.
The clause to write for weight on 3D mesh
The line below is the version we can quote against without inventing anything. Weight appears with a tolerance and a test, not as a standalone number.
Write it once and reuse it. The buyers who avoid claims are not stricter than everyone else; they send the same well-written clause every time.
How to write a 3D mesh specification that protects you
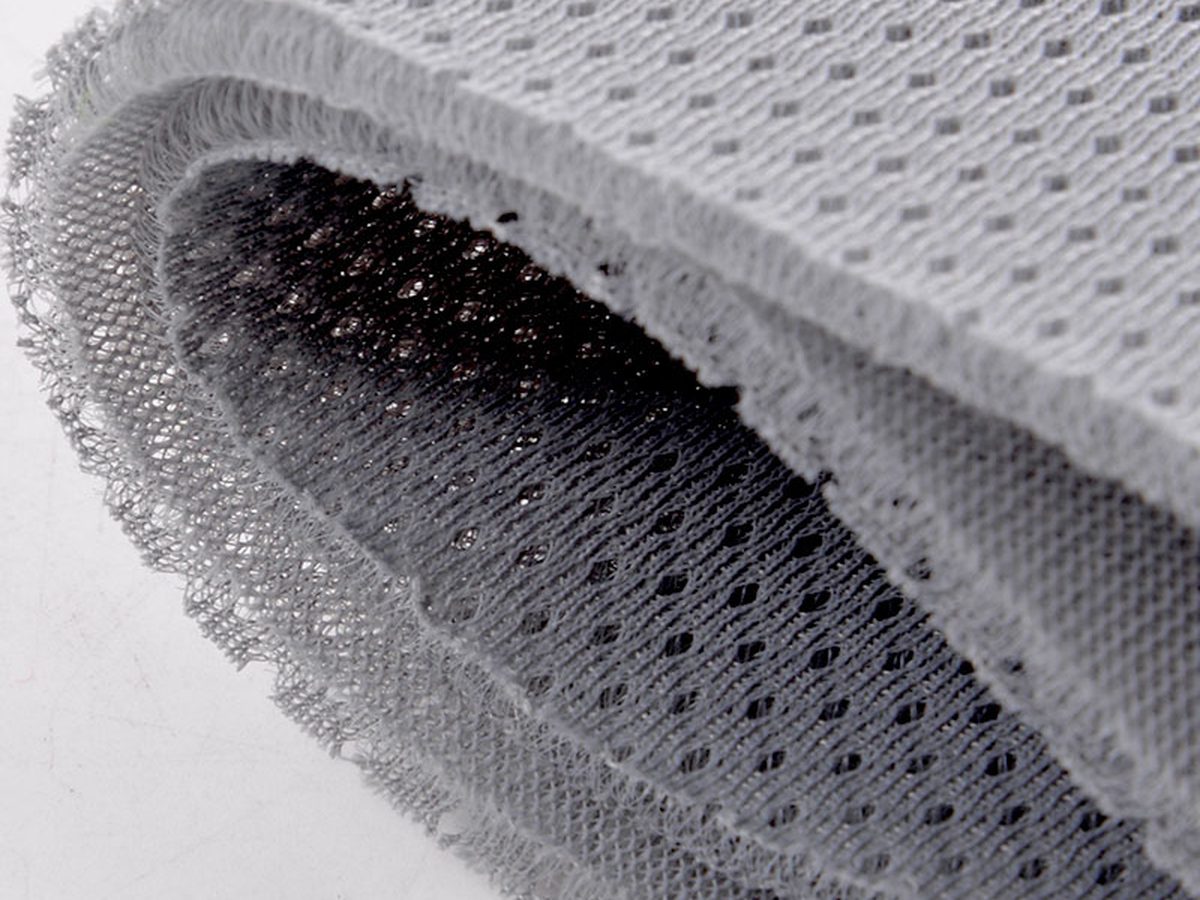
A specification is only useful if a substitution becomes visible. That means writing the construction and the performance together, and naming the test that proves each one. For 3D mesh, the clause has to pin compression recovery and air permeability, because those two separate a compliant lot from an adequate one:
3D spacer mesh, 100 % polyester, 6 mm, 320 gsm, 155 cm usable, compression recovery >= 90 %, laminated to 2 mm PU foam with hot-melt adhesive, Pantone 19-4013 TCX
Note what is missing from that line: adjectives. No ‘high quality’, no ‘premium’, no ‘export grade’. Every clause is either a number with a tolerance or a named test. If a supplier cannot quote against a line written this way, that is information about the supplier.
3D mesh: where the specification usually breaks down
The first failure is compression set. Seat pads flatten in the first months; foam looks tired while the cover is intact. The cause is usually monofilament too thin or density too low for the load, or the wrong polymer for the climate. The test that exposes it before you order: Load a 100 mm square with 5 kg at 40 C for 24 h, release, measure recovery after 30 min.
The second is delamination. Mesh separates from foam or backing after washing or dry cleaning. It comes from flame lamination is cheap and fails at the adhesive line under heat and solvent. Test with ISO 2411 peel strength on a 50 mm strip, before and after one wash cycle. and write the result into the purchase order, not just the enquiry.
Both failures share a pattern: they appear months after delivery, they are hard to attribute, and the cost lands on the buyer rather than the mill. That is exactly why the test belongs in the specification and the report belongs in the shipment file.
What to put in a 3D mesh enquiry
- End use and the conditions, which together decide where compression recovery has to sit inside >= 90 %.
- The one figure that must hold, with compression recovery named as the proof.
- Quantity per colour and per delivery, against a typical MOQ of 300-500 m per colour.
- Destination market, because compliance changes the construction, not just the paperwork On 3D mesh that is thickness at 3-15 mm.
- A physical standard viewed under a stated light source, not a screen proof For 3D mesh fabric it is weight at 180-420 gsm that settles it.
With those five points we can quote against a real requirement instead of a generic range. Full ranges sit on the 3D mesh page, and the manufacturing side of the same question is on our quality control page.

Questions buyers ask before ordering
Is 3-15 mm a limit or a typical value for specification explained?
On specification explained, the number to quote is 3-15 mm.
What is the actual tolerance behind specification explained?
On specification explained, ask for 3-15 mm in writing.
Can you hold tolerance at 3-15 mm for specification explained on a repeat order?
On specification explained, on this item the tolerance sits at 3-15 mm.
3D mesh: failure modes worth a clause in the purchase order
| Failure | What triggers it | Test to demand on the production lot | Compression set | Monofilament too thin or density too low for the load, or the wrong polymer for the climate. | Compression recovery — internal 5 kg / 24 h / 40 C; acceptance >= 90 % | Delamination | Flame lamination is cheap and fails at the adhesive line under heat and solvent. | Peel strength (laminated) — ISO 2411; acceptance >= 6 N/50 mm |
|---|
The other two, with acceptance numbers attached, are in the full failure analysis for 3D mesh. A supplier who cannot name the mode he sees most often is describing a catalogue, not a process.
Need 3D mesh quoted against your specification?
Send the thickness and the destination market. The reply states the range we hold, the price at that volume, and which test report travels with the goods.
Products in this range
Related reading
- Sportswear and activewear: Materials, Specifications and Failure Risks
- How to Compare Supplier Quotes That Look Nothing Alike
- Bags Fabric Sourcing: 600D vs 1680D, Coating and Seam Failure
Sample cut with your values on it · Neutral packing and private label · Consolidation, documents and lead times