A non-woven fabric claim almost never arrives in the first month. It arrives after a season, in a specific climate, on a specific batch. The four patterns below account for most of them.
Non-woven: why failures cluster around one or two parameters
In non-woven, the parameters in the table below are not independent. Tensile strength and Elongation between them explain most field failures, and both are routinely omitted from quotations because they are expensive to guarantee and easy to leave vague.
| Parameter | Typical range | Why it decides failure | Tensile strength | MD 20-60 N/5 cm | Direction matters: CD strength is usually half of MD and fails first. | Elongation | 20-80 % | Low elongation is brittle; high elongation bags out. | Width | 160-320 cm | Wide goods reduce seams on covers and bags. | Hydrophilic / hydrophobic | specified, not assumed | A ‘breathable’ claim usually depends on this treatment. |
|---|
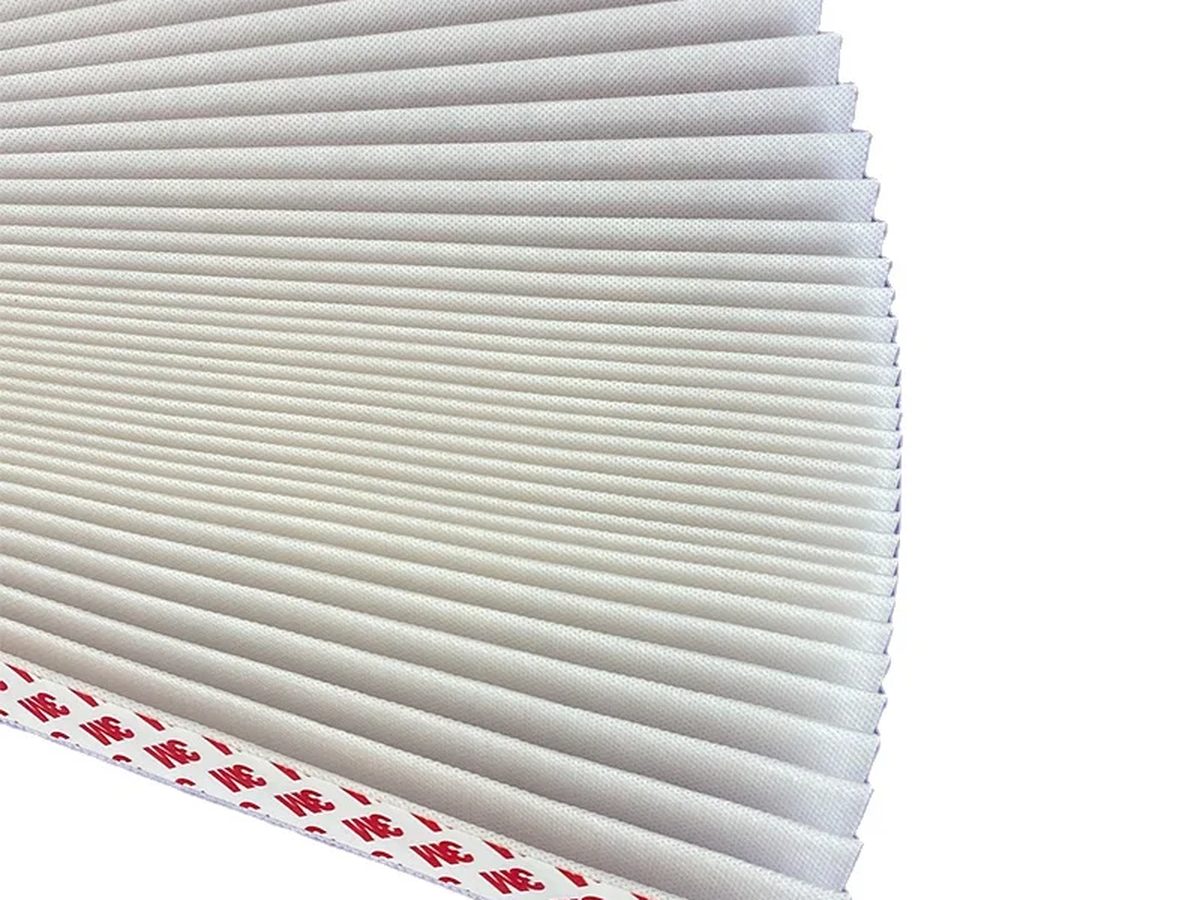
1. Low CD strength
What you see. Material tears across the roll when pulled or sewn.
Why it happens. Fibre orientation biased to machine direction, typical of cheap spunbond.
Tensile MD and CD per ISO 9073-3; require both figures.
What to specify instead. Specify a CD:MD ratio above 0.6, or choose a cross-laid process.
2. Weight shortfall
What you see. The roll weighs less than ordered and the cover feels thin.
Why it happens. Nominal gsm quoted from the line setting, not the delivered goods.
ISO 9073-1 mass per unit area on three samples per lot.
What to specify instead. Buy on measured gsm with a +/- 5 % tolerance written into the PO.
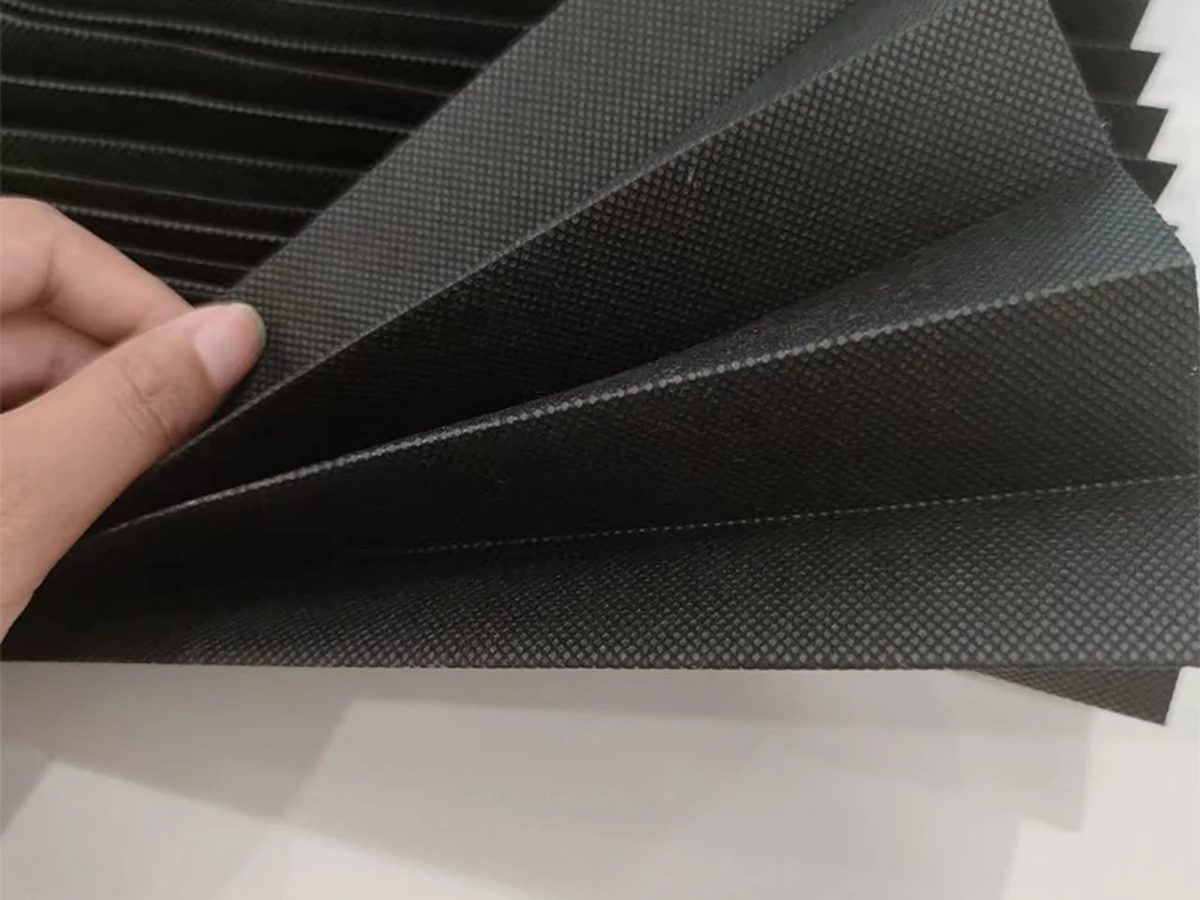
3. Colour lot variation
What you see. Bags from two lots read as two different products.
Why it happens. Surface dyeing at low gsm; poor bath control.
Visual under D65 plus dE measurement.
What to specify instead. Solution-dyed for dark shades and any multi-lot order.
4. Edge fraying
Why it happens. Needle-punch or spunbond without edge sealing.
Manual rub test and a tape-lift test on cut edges.
What to specify instead. Ultrasonic or heat-sealed edges for clean-room and medical-adjacent uses.
Non-woven: building a test plan you will actually run
| Test | Method | Acceptance | Mass per unit area | ISO 9073-1 | +/- 5 % of nominal | Tensile strength | ISO 9073-3 | MD >= 20 N/5 cm, CD >= 12 N/5 cm | Elongation | ISO 9073-3 | report MD and CD | Tear resistance | ISO 9073-4 | report | Colour fastness to rubbing; measured on process, spunbond, spunlace, needle punch or SMS | ISO 105-X12 | >= grade 3-4 |
|---|
Non-woven: what the report should contain
- Process spunbond, spunlace, needle punch or SMS — measured at three positions on the roll, recorded as a number rather than pass or fail On non-woven that is process at spunbond, spunlace, needle punch or SMS.
- Weight 15-200 gsm — cut from the middle of the lot, not from the end of the roll For non-woven fabric it is weight at 15-200 gsm that settles it.
- Tensile strength 20-60 N/5 cm in MD — read at 23 C / 50 % RH after conditioning, not straight off the machine On non-woven, skipping this is what produces cross-direction tear at the seam.
- Elongation 20-80 % — checked on production material, at in-process rather than only at pre-shipment For non-woven fabric, the figure to write down is tensile strength at 20-60 N/5 cm in MD.
- Width 160-320 cm — stated in the purchase order with the test method beside it On non-woven that is process at spunbond, spunlace, needle punch or SMS.
- ISO 9073-3 for tensile, ISO 9073-4 for tear, EN 29073 for mass per unit area — run to the method named above; the report travels with the lot For non-woven fabric it is weight at 15-200 gsm that settles it.
Specification ranges for non-woven are on the product page.
Questions buyers ask before ordering
What drives the price of failure modes and tests at tolerance of 20-60 n?
On failure modes and tests, the answer is 20-60 n, and the reason is the heat setting.
Is 20-60 n achievable at our volume on failure modes and tests?
On failure modes and tests, our standard is 20-60 n, verified by lab certificate.
How do you verify tolerance against 20-60 n on failure modes and tests?
On failure modes and tests, the number to quote is 20-60 n.
The test plan for non-woven
The minimum set on non-woven
| Test | Method | Acceptance | Mass per unit area | ISO 9073-1 | +/- 5 % of nominal | Tensile strength | ISO 9073-3 | MD >= 20 N/5 cm, CD >= 12 N/5 cm | Elongation | ISO 9073-3 | report MD and CD | Tear resistance | ISO 9073-4 | report | Colour fastness to rubbing; held at process, spunbond, spunlace, needle punch or SMS | ISO 105-X12 | >= grade 3-4 | Hydrostatic head (SMS) | ISO 811 | >= 300 mm for barrier uses |
|---|
Sampling for non-woven, and where it goes wrong
For a first order of non-woven, take three positions along the run and one sample per colour, then test mass per unit area on all of them rather than on a composite.
Several non-woven results move by 10-20 % between a dry laboratory and a humid one, which is why two labs can disagree on the same material without either being wrong.
Reading a non-woven report properly
- Process spunbond, spunlace, needle punch or SMS — measured at three positions on the roll, recorded as a number rather than pass or fail On non-woven, skipping this is what produces cross-direction tear at the seam.
- Weight 15-200 gsm — cut from the middle of the lot, not from the end of the roll For non-woven fabric, the figure to write down is tensile strength at 20-60 N/5 cm in MD.
- Tensile strength 20-60 N/5 cm in MD — read at 23 C / 50 % RH after conditioning, not straight off the machine On non-woven that is process at spunbond, spunlace, needle punch or SMS.
- Elongation 20-80 % — checked on production material, at in-process rather than only at pre-shipment For non-woven fabric it is weight at 15-200 gsm that settles it.
- Width 160-320 cm — stated in the purchase order with the test method beside it On non-woven, skipping this is what produces cross-direction tear at the seam.
- ISO 9073-3 for tensile, ISO 9073-4 for tear, EN 29073 for mass per unit area — run to the method named above; the report travels with the lot For non-woven fabric, the figure to write down is tensile strength at 20-60 N/5 cm in MD.
The three tests buyers skip and regret on non-woven
For non-woven that usually means tensile strength measured after the wash or exposure the product will actually see, because low cd strength does not appear in a conditioned laboratory.
Weight shortfall is usually a construction failure rather than a material one.
Third, retention. It is the only way to know whether tensile strength changed or the conditions did.
Turning test results into a purchase order clause on non-woven
Full parameter ranges are on the non-woven page; the checks that hold those ranges in production are described on the quality control page.
How often to re-test on non-woven
| Stage | What to test | Frequency | Development sample | All parameters in the specification; read against process, spunbond, spunlace, needle punch or SMS | Once per development | First production lot | All parameters, plus the end-use test; written as process spunbond, spunlace, needle punch or SMS | Every lot for the first three; measured on process, spunbond, spunlace, needle punch or SMS | Repeat lots | Critical parameters and the one that failed before; held at process, spunbond, spunlace, needle punch or SMS | Every lot | Annual | Full panel, including ageing where relevant; read against process, spunbond, spunlace, needle punch or SMS | Once a year, or after any process change; written as process spunbond, spunlace, needle punch or SMS |
|---|
Retained samples: the cheapest insurance in the order on non-woven
For non-woven, the sample should include the finish, not just the base material, because low cd strength usually starts in the finish or the additive rather than the substrate.
The test plan for non-woven, by order size
| Order | Tests to run | What it establishes | Sample or trial | Mass per unit area | Whether the material can meet the requirement at all; measured on process, spunbond, spunlace, needle punch or SMS | First production order | Mass per unit area, Tensile strength, Elongation | The baseline every later lot is compared against; held at process, spunbond, spunlace, needle punch or SMS | Repeat orders | Mass per unit area plus the parameter that failed last time | Whether the process has drifted; read against process, spunbond, spunlace, needle punch or SMS | Annual or after a process change; written as process spunbond, spunlace, needle punch or SMS | Full panel | That nothing has moved in the background; measured on process, spunbond, spunlace, needle punch or SMS |
|---|
For non-woven, the one test never worth dropping is mass per unit area, because it is the one that predicts low cd strength.
The claim file for non-woven, and how long to keep it
Claims on non-woven fabric are lost on documentation far more often than on material. By the time cross-direction tear at the seam appears, the sample is gone and the non-woven lot is cut, so the file is the case.
- The signed specification, with process at spunbond, spunlace, needle punch or SMS and weight at 15-200 gsm on the same page as the non-woven price.
- The sealed bulk approval sample for non-woven, dated — not the development sample.
- The lot record showing process as measured on non-woven fabric, not as passed.
- Photographs of the non-woven consignment at goods-in, before the material was cut.
- The non-woven inspection report naming the method: ISO 9073-3 for tensile, ISO 9073-4 for tear, EN 29073 for mass per unit area.
Keep the non-woven file for the warranty period plus one season — usually 24 months in export. A shelf costs nothing; a non-woven shipment without the file costs the whole order.
Two of the five are almost always missing on non-woven, and they are the two that decide it: the bulk approval sample and the measured process value.
Want a non-woven quotation you can compare line by line?
Tell us the weight and the annual volume. The quotation comes back with the tolerance band, the MOQ per colour, and the test standard named against each figure.
Products in this range
Related reading
- Knitted Fabric vs Woven shirting: Which One Fits Your Programme
- Shipping Textile and Window Covering from China: Container Maths, Packaging and Damage Control
- Wooden Blind Slat Specification Guide: Species, Moisture and Tolerance
Sample cut with your values on it · Neutral packing and private label · Consolidation, documents and lead times